lvobo blog
Home

powder quality control

powder quality control

  • Why Your Sieve Analysis Results May Be Wrong Before Testing Begins
    Why Your Sieve Analysis Results May Be Wrong Before Testing Begins
    Nov 12, 2026
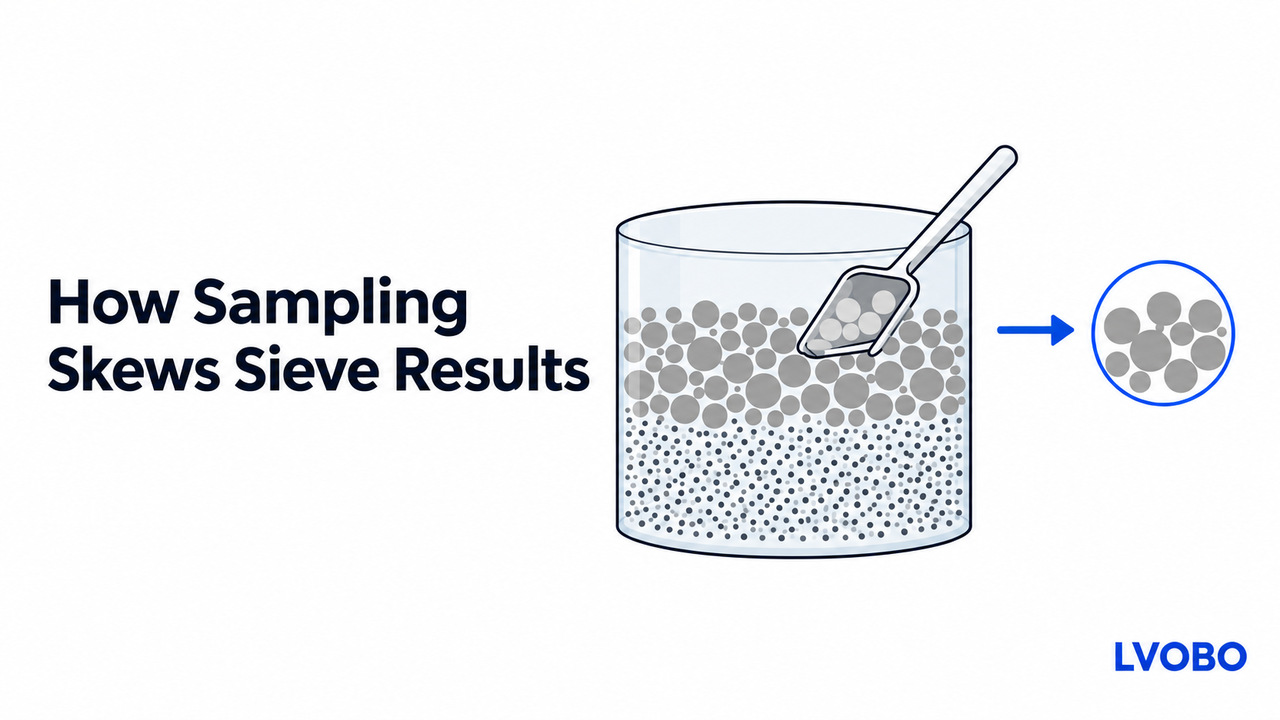
    A Sieve Test Can Be Inaccurate Before the Machine Starts When sieve analysis results vary between tests, laboratories often begin by checking the sieve mesh, vibration settings, or screening duration. However, the source of the problem may exist before the sample reaches the sieve shaker. Powders can segregate during transportation, storage, and handling. Differences in particle size, density, shape, and surface properties may cause coarse and fine particles to become unevenly distributed within a container. If a technician collects a test portion from only one accessible location, the sample may not represent the original batch. For QC engineers and procurement teams, representative sampling is an essential part of particle size analysis, not simply a preliminary handling step. A properly operated sieve shaker cannot compensate for a sample that does not represent the material being tested. How the Brazil Nut Effect Causes Powder Segregation One well-known example of granular segregation is the Brazil Nut Effect. When a mixture of particles experiences repeated vibration or movement, larger particles may migrate toward the upper region while smaller particles move into the spaces below. This phenomenon is familiar from a container of mixed nuts: larger nuts often appear near the top after transportation or shaking. A similar effect can occur in industrial powders and granular materials. However, particle segregation is more complex than simply saying that large particles always rise. Several factors influence particle movement: Particle Size Ratio: Differences in particle dimensions affect how smaller particles move through spaces between larger ones. Density Contrast: Differences in particle density can influence the direction and rate of segregation. Particle Shape: Irregular and elongated particles may move differently from spherical particles. Vibration Conditions: Frequency, amplitude, vibration intensity, and duration can influence particle migration. Surface and Environmental Conditions: Friction, moisture, cohesion, and container geometry can also affect segregation. Under certain conditions, the opposite behavior, known as the Reverse Brazil Nut Effect, can occur, causing larger particles to migrate downward. There is no universal rule that predicts segregation direction from vibration frequency or density alone. These variables interact with the particle system and operating conditions. Why Does This Matter for Laboratory Testing? A sample collected from the top of a container may contain a different proportion of coarse and fine particles than one collected from the middle or bottom. The resulting particle size distribution may therefore reflect the sampling location rather than the actual composition of the entire batch. 4 Common Sampling Mistakes That Distort Sieve Analysis Results Even when the sieve shaker operates correctly, poor sampling practices can introduce significant variation. The following comparison highlights four common mistakes, their consequences, and the corresponding corrective procedures. Mistake Consequence Correct SOP Top-Surface SamplingCollecting powder only from the top of a bag or drum. The sample may contain an unrepresentative proportion of coarse or fine particles due to segregation. Collect increments from multiple representative locations using a suitable sampling device or defined sampling procedure. Single Grab SamplingTaking one scoop from one accessible location. Local particle distribution may not represent the entire production batch. Collect multiple increments and combine them into a composite sample when appropriate. Ignoring Transportation EffectsOverlooking vibration, handling, and storage history. Previously uniform powders may become segregated during transportation or storage. Document material history and apply a validated sampling or homogenization procedure where necessary. Uncontrolled Sample SplittingReducing bulk material through arbitrary scooping or unsuitable manual methods. Coarse and fine fractions may become unevenly distributed in the final test portion. Use a suitable riffle splitter, chute splitter, or rotary sample divider where appropriate. Validate the splitting method for the material. QC Consideration: Traditional cone-and-quartering is not automatically unsuitable. However, for fine, cohesive, electrostatic, or segregation-prone powders, manual splitting may introduce additional operator-dependent variation. A suitable mechanical divider can provide better control when its use has been validated. 5 Steps to Obtain a More Representative Powder Sample A reliable sieve analysis procedure begins with controlled sampling and sample preparation. Step 1: Collect Samples from Representative Locations Whenever practical, sample powder while it is moving during transfer or discharge. Collect multiple small increments across the material stream rather than relying on one large scoop from a single location. For packaged materials, use a suitable sampling device that can reach defined positions within the container. Step 2: Prepare a Composite Sample Combine the collected increments to form a representative primary sample. This helps account for variations between different sampling locations or collection times. Step 3: Reduce the Sample Using a Suitable Divider Use a suitable riffle divider, chute splitter, or rotary sample divider to obtain the required test portion. The objective is to preserve the relative proportions of different particle fractions during sample reduction. For fine or cohesive powders, verify that the selected divider does not introduce material loss, blockage, or additional segregation. Step 4: Prevent Loss of Fine Particles Fine particles may be lost during transfer, remain attached to container surfaces, or become airborne during handling. Use clean, suitable containers and controlled transfer procedures. Protect samples from moisture changes, contamination, and unnecessary material loss. Even small changes in sample composition can influence the reported particle size distribution. Step 5: Verify Results Using Independently Prepared Test Portions If repeated sieve tests produce substantially different results, prepare additional test portions using the same controlled sampling and splitting procedure. Compare the results before assuming that the sieve shaker requires recalibration. This helps distinguish sampling variation from differences in the screening process. What a Laboratory Sieve Shaker Can—and Cannot—Control Representative sampling establishes the quality of the test portion. The next step is to control the mechanical screening process itself. Even when a sample is properly prepared, inconsistent equipment motion, screening duration, or operating procedures can introduce additional variation. Controlled mechanical vibration helps reduce equipment-related testing variation by making screening conditions more consistent and repeatable. A laboratory sieve shaker can control important operating conditions, but it cannot correct an unrepresentative sample or guarantee identical results for every material. For this reason, sample preparation and sieve operation should be managed as two separate quality control stages. Repeatable Screening with LVOBO Laboratory Sieve Shakers Once sampling representativeness has been established, selecting equipment with controllable and repeatable mechanical motion becomes the second important step. LVOBO laboratory sieve shakers, including the BO-200SY and BO-300SY, are designed for laboratory particle size analysis, powder classification, and sieve residue testing. The upgraded BO-SY control system provides several functions to help laboratories standardize screening procedures. Forward and Reverse Motion: Adjustable forward and reverse motion modes allow laboratories to configure different screening patterns according to material characteristics and testing requirements. Adjustable Vertical Vibration: Vertical vibration intensity can be adjusted to accommodate different powder screening requirements. Programmable Screening Procedures: The touchscreen controller allows users to configure operating time, cycle settings, and motion conditions for different materials. 21 Screening Program Memories: Up to 21 screening programs can be stored and recalled, helping laboratories maintain consistent operating procedures across different samples, operators, and testing sessions. These functions help laboratories control the mechanical screening stage after a suitable test portion has been prepared. The objective is not to compensate for poor sampling, but to reduce variation caused by inconsistent screening conditions. Pre-Test QC Checklist for Laboratory Engineers Before starting a sieve analysis test, review these five conditions: ☐ Sampling Location: Was the sample collected from representative locations rather than only from the container surface? ☐ Transportation History: Could vibration, handling, or storage have caused particle segregation? ☐ Sample Mass: Is the test portion appropriate for the material and selected sieve procedure? ☐ Sample Reduction: Was the test portion prepared using a suitable and controlled splitting method? ☐ Testing Conditions: Are sieve apertures, motion settings, screening duration, and operating procedures defined? If any of these conditions are uncertain, investigate them before attributing inconsistent results to the sieve shaker. Reliable Sieve Analysis Starts Before Screening Accurate particle size analysis depends on more than a calibrated sieve stack. Sampling procedures, particle segregation, sample reduction, and material handling all influence the quality of the test portion. The Brazil Nut Effect demonstrates how granular materials can change their spatial distribution during transportation and vibration. First, prepare a representative sample. Second, establish controlled mechanical screening conditions. By standardizing both stages, laboratories can improve the reliability of batch comparisons, supplier qualification, incoming material inspection, and powder quality control. Technical References ISO 14488:2007 — Particulate materials: Sampling and sample splitting for the determination of particulate properties. ASTM E2651-25 — Standard Guide for Powder Particle Size Analysis. ASTM B215-20(2025) — Standard Practices for Sampling Metal Powders.
    Read More
  • Particle Size vs. Particle Shape: Why Sieve Analysis Is Only the Starting Point
    Particle Size vs. Particle Shape: Why Sieve Analysis Is Only the Starting Point
    Nov 01, 2026
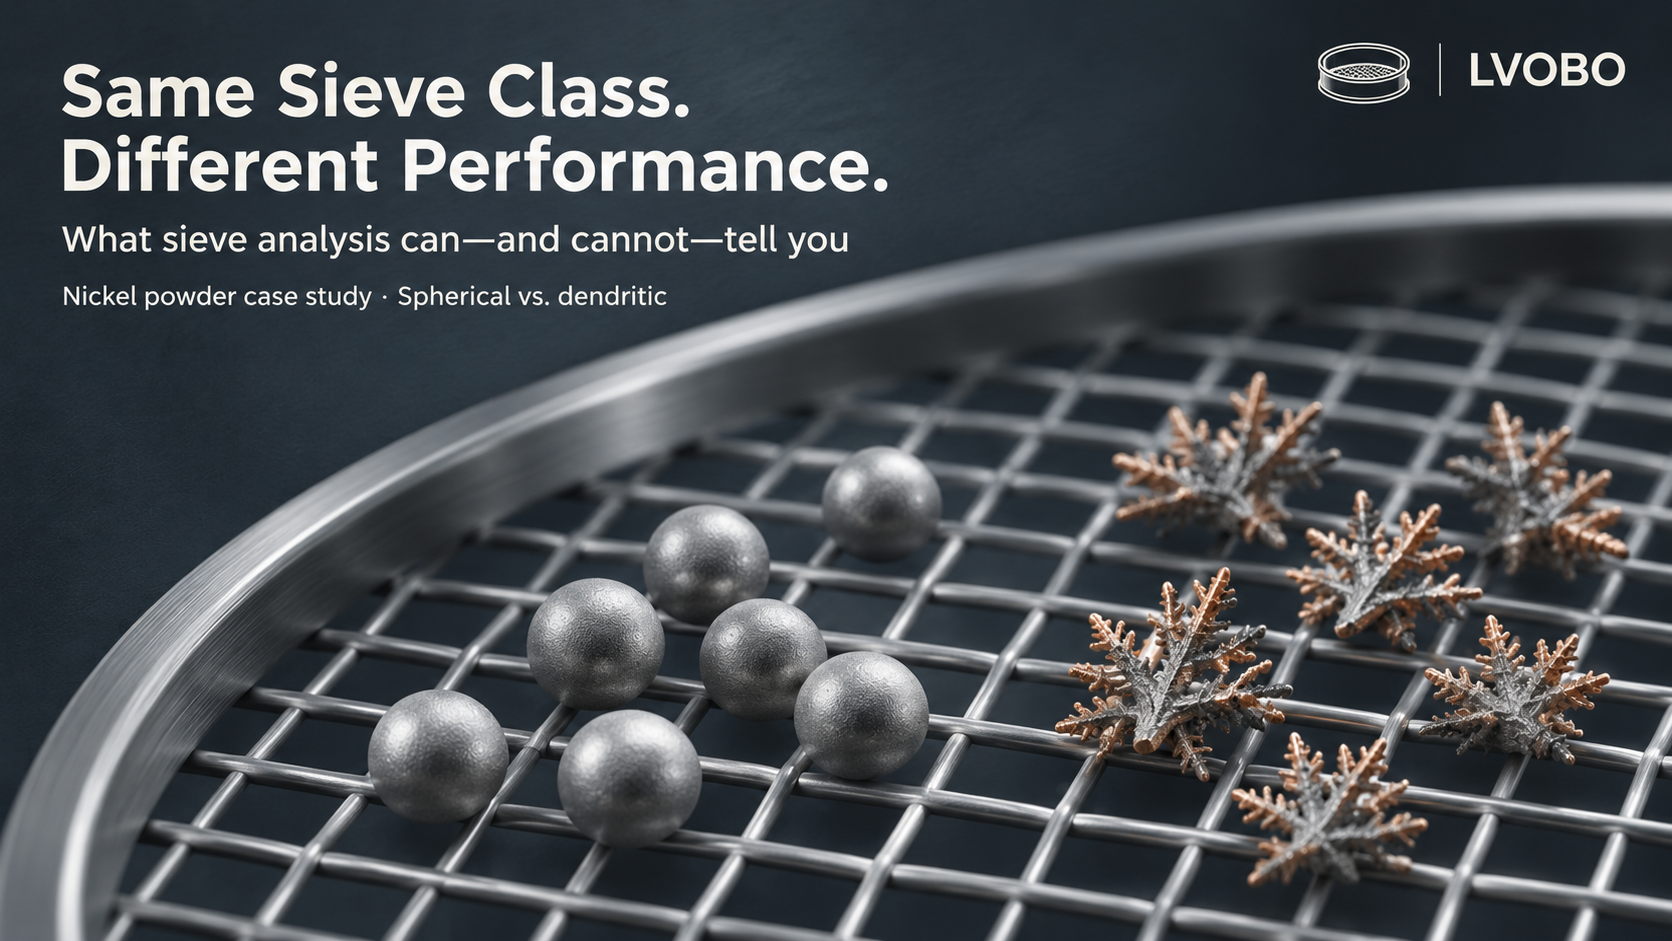
    In powder procurement and quality control, particle size is often the first metric written into a specification. Once the powder passes through the sieve, falls into the specified size fraction, and the report shows "Pass," the process for many stops there. But here is the question: Does particle size compliance truly equal powder performance compliance? A recent 2026 study on commercial nickel powders by a South Korean research team, published in the Journal of Powder Materials, offers a blunt reminder: Not necessarily. The researchers compared spherical and dendritic nickel powders, further dividing each morphology into two sieve classes: 25–32 μm and 32–45 μm. They found that within the tested sample groups, changing the sieve classification had a relatively limited impact on resistivity, while the difference in electrical behavior between the spherical and dendritic groups was striking. Under matched pressure conditions, the reported resistivity values differed by a factor of approximately 16 to 70, depending on the pressure conditions and sample pairs. This is not to say sieving is unimportant. Sieving is, of course, crucial—it is a fundamental tool for particle size control. But it answers a very narrow question: Can this powder pass through this sieve aperture, and which size fraction does it fall into? It does not answer whether the particles are spherical or dendritic, whether the surface is oxidized, whether the supplier's process is consistent, and it certainly does not answer how this powder will actually perform in pressure-conductive rubber. The Core Pain Point of Sieve Reports: It Looks Too Much Like a "Complete Answer" Sieving analysis is highly practical in the lab. It can tell you: The mass retained on each sieve aperture; The proportion of material within the specified size fraction; The presence of oversized particles; Whether there are variations in particle size distribution between batches; Whether the powder meets sieve-based acceptance criteria. This information is valuable. The problem is that many procurement and quality processes equate "meeting sieve acceptance criteria" directly with "stable powder quality." This is a dangerous leap. Powders within the same sieve class can be completely different in the following aspects: Particle morphology: spherical, dendritic, irregular, or flake-like; Surface structure: roughness, oxide layer, surface treatment; Inter-particle contact mode: point contact, surface contact, branched interlocking; Specific surface area and flowability; Resistivity, filling behavior, or processing performance in actual applications. A sieve report won't tell you these things. It cannot independently determine whether particles are spherical or dendritic, cannot quantify surface roughness, cannot identify surface oxidation, and cannot measure resistivity. Using sieve analysis for these tasks is like using a bathroom scale to judge a person's health—weight matters, but it’s not the whole story. What's Really Striking About This South Korean Nickel Powder Study: Same Sieve Class, Performance Can Differ by an Order of Magnitude The study focused on nickel powders used in pressure-conductive rubber semiconductor test sockets. The researchers compared four commercial nickel powder samples with two morphologies: spherical and dendritic; each morphology was further divided into two sieve classes: 25–32 μm and 32–45 μm. They evaluated particle size distribution, surface area, true density, particle morphology, and resistivity under different compression pressures. The results are clear: within the tested sample groups, sieve class variation had a relatively limited impact on resistivity, while the difference between the spherical and dendritic groups was very large. Dendritic powders exhibited lower resistivity or formed effective conductive contacts earlier at lower compression pressures; under matched pressure conditions, the resistivity of the two groups differed by a factor of approximately 16 to 70. A crucial caveat must be stated: the spherical and dendritic powders came from different suppliers. Therefore, this difference is a combined effect of morphology and supplier factors, and cannot prove that particle morphology alone caused all the differences. The supplier's manufacturing process, surface state, impurity control, and oxidation degree may all play a role. But it is precisely this caveat that makes the conclusion even more impactful for procurement and quality control: the sieve report you receive doesn't even cover the variables that truly affect performance—"morphology + supplier + surface state." Particle size compliance might just be "looking compliant." Even More Provocative: Sieve and Laser Diffraction Results Might Naturally Be Inconsistent The study includes an interesting detail. The researchers first separated the nickel powder into a 25–32 μm sieve class, then measured the particle size distribution using laser diffraction. The reported laser diffraction D50 values for the spherical and dendritic samples were approximately 34.9 μm and 35.5 μm, respectively. At first glance, this seems contradictory to the sieve class. But it’s not that sieving must be wrong; rather, the two methods measure different things. Mechanical sieving looks at whether a particle can pass through a sieve aperture under specified conditions; for non-spherical particles, passage depends on the effective cross-section and orientation. Laser diffraction calculates an equivalent spherical diameter; an elongated or branched particle might pass through a sieve aperture in a favorable orientation but yield a larger equivalent spherical diameter in laser diffraction. D50 is the median equivalent spherical diameter, not the sieve upper limit. Therefore, inconsistency between sieve and laser diffraction results does not automatically mean a testing error. It just reminds you that different measurement principles answer different questions. For powder engineers, when comparing supplier reports, if the particle size analysis methods differ, directly comparing the numbers is risky. What Sieve Analysis Should and Should Not Do Sieve analysis should continue to be done, and done well. It is a fundamental tool for laboratory particle size analysis and quality control. But it should not be treated as a complete evaluation of powder performance. Sieve analysis confirms particle size distribution and sieve residue; it cannot replace SEM for morphology, image analysis for shape quantification, surface analysis for oxidation, or application testing for resistivity, flowability, or filling behavior. A more reasonable powder evaluation workflow should be divided into three layers: Particle Size Classification: Use test sieves and controlled screening procedures to confirm size fractions, retained mass, and oversized particles. Particle Morphology: Use microscopy or image analysis to check if particles are spherical, dendritic, or irregular, and whether the surface structure is consistent. Application-Specific Performance: Directly measure metrics relevant to the application scenario, such as resistivity, flowability, surface area, and chemical composition. Not every powder requires all three layers. But if your application is sensitive to morphology, contact structure, or electrical conductivity, looking only at a sieve report is far from enough. The Role of Laboratory Sieve Shakers: Do Particle Size Control Solidly, But Don't Make It Take the Blame It Shouldn't For laboratories handling metal powders, chemical powders, pharmaceutical materials, and advanced materials, laboratory sieve shakers remain core equipment for particle size control. Compared to manual sieving, programmable laboratory sieve shakers standardize mechanical motion, operating time, and testing procedures, making sieve results between batches more comparable. LVOBO laboratory sieve shakers, including the BO-200SY and BO-300SY models, are designed for laboratory particle size analysis, powder classification, and sieve residue testing. Selected configurations offer programmable screening functions such as forward/reverse motion, vertical vibration control, operating time and cycle settings, and storage for multiple test programs; specific functions depend on the configuration. But the equipment's role must be clearly stated: a sieve shaker determines how material passes through selected apertures; it does not replace SEM, image analysis, surface analysis, or resistivity testing. It is the starting point of particle size control, not the endpoint of powder quality. Using the sieve shaker correctly means controlling the particle size variable; treating the sieve report as a complete quality conclusion leaves the risk to downstream processes. Conclusion: Particle Size Compliance is Just the Starting Point, Not the Endpoint The core takeaway from this South Korean nickel powder study for procurement engineers, R&D teams, and quality control labs is: powders within the same sieve class can still exhibit significantly different behaviors in specific applications. And because morphology and supplier factors were confounded in the study, this result serves more as a warning: do not treat a sieve class as a complete quality description, and do not assume a sieve report covers morphology, surface state, and supplier consistency. So, to put it boldly: Sieve analysis is a must, but judging powder quality solely by sieve analysis is like using one ruler to measure an entire material system. Use sieving to control particle size, use microscopy and image analysis to examine morphology, and use application testing to evaluate actual performance. Reliable powder quality control is not about buying more instruments; it's about understanding exactly what questions each method can and cannot answer. Particle size compliance is just the starting point. True powder quality lies beyond the sieve apertures.
    Read More

leave a message

leave a message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
Submit

Our hours

Monday - Saturday: 8:00 AM - 6:00 PM

Contact Us:lvobo2026@gmail.com

Home

Products

whatsApp

contact